Define
Translate component requirements into controlled instructions.
 Discuss a component
QUALITY AND TRACEABILITY
The environment, work instruction, inspection result and lot record must describe the same component and the same agreed method.
Follow the evidence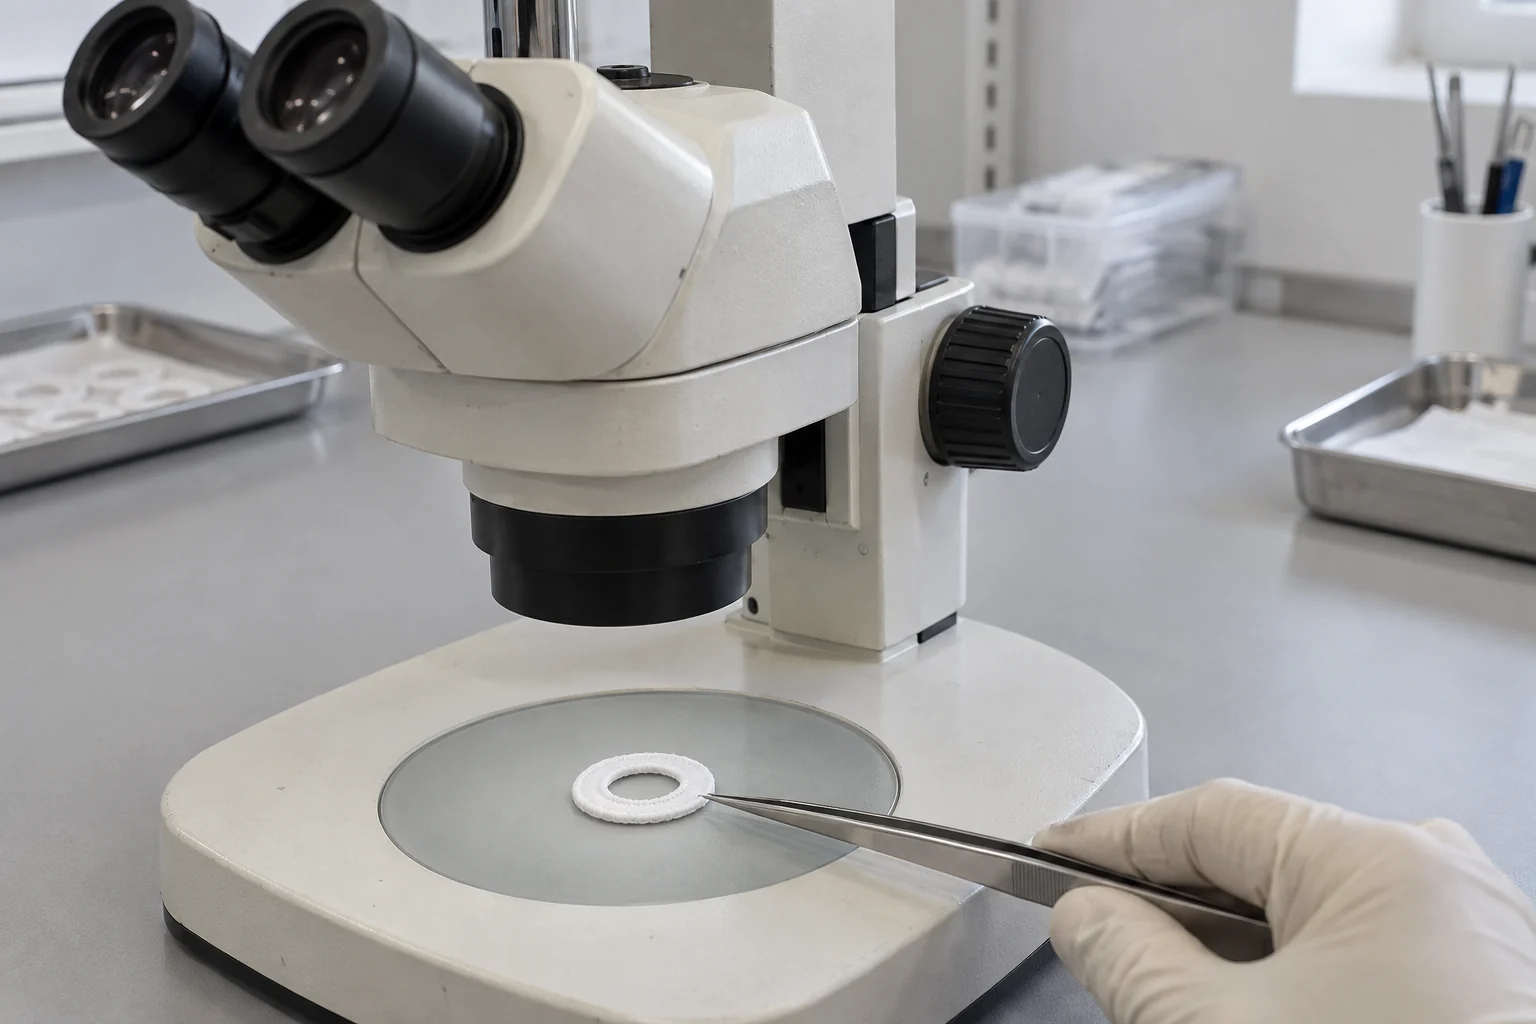
THE EVIDENCE CHAIN
Quality does not begin at final inspection. It starts when component requirements become controlled instructions and continues through every recorded step.
Controlled entry, filtered air, gowning and cleaning routines support the assembly environment.
THE CONTROLLED METHOD
Translate component requirements into controlled instructions.
Follow the agreed material, preparation and sewing sequence.
Check the component against visual and dimensional criteria.
Connect materials, work and inspection results at lot level.
DEFINING THE CHECKS
AJSM’s process-development work includes defining quality checks around the actual component. The drawing, materials and agreed assembly method determine what needs to be inspected.
These are review topics, not universal pass/fail limits. The device manufacturer and AJSM agree the checks, handling and packaging requirements before the programme moves forward.
Read the guide to connected recordsPARTNER QUALIFICATION
Customer audits, pilot lots and acceptance criteria form a proposed qualification route. The exact sequence is agreed for the component programme.
This page describes AJSM’s current approach. It does not claim completed customer qualification or ISO 13485 certification.
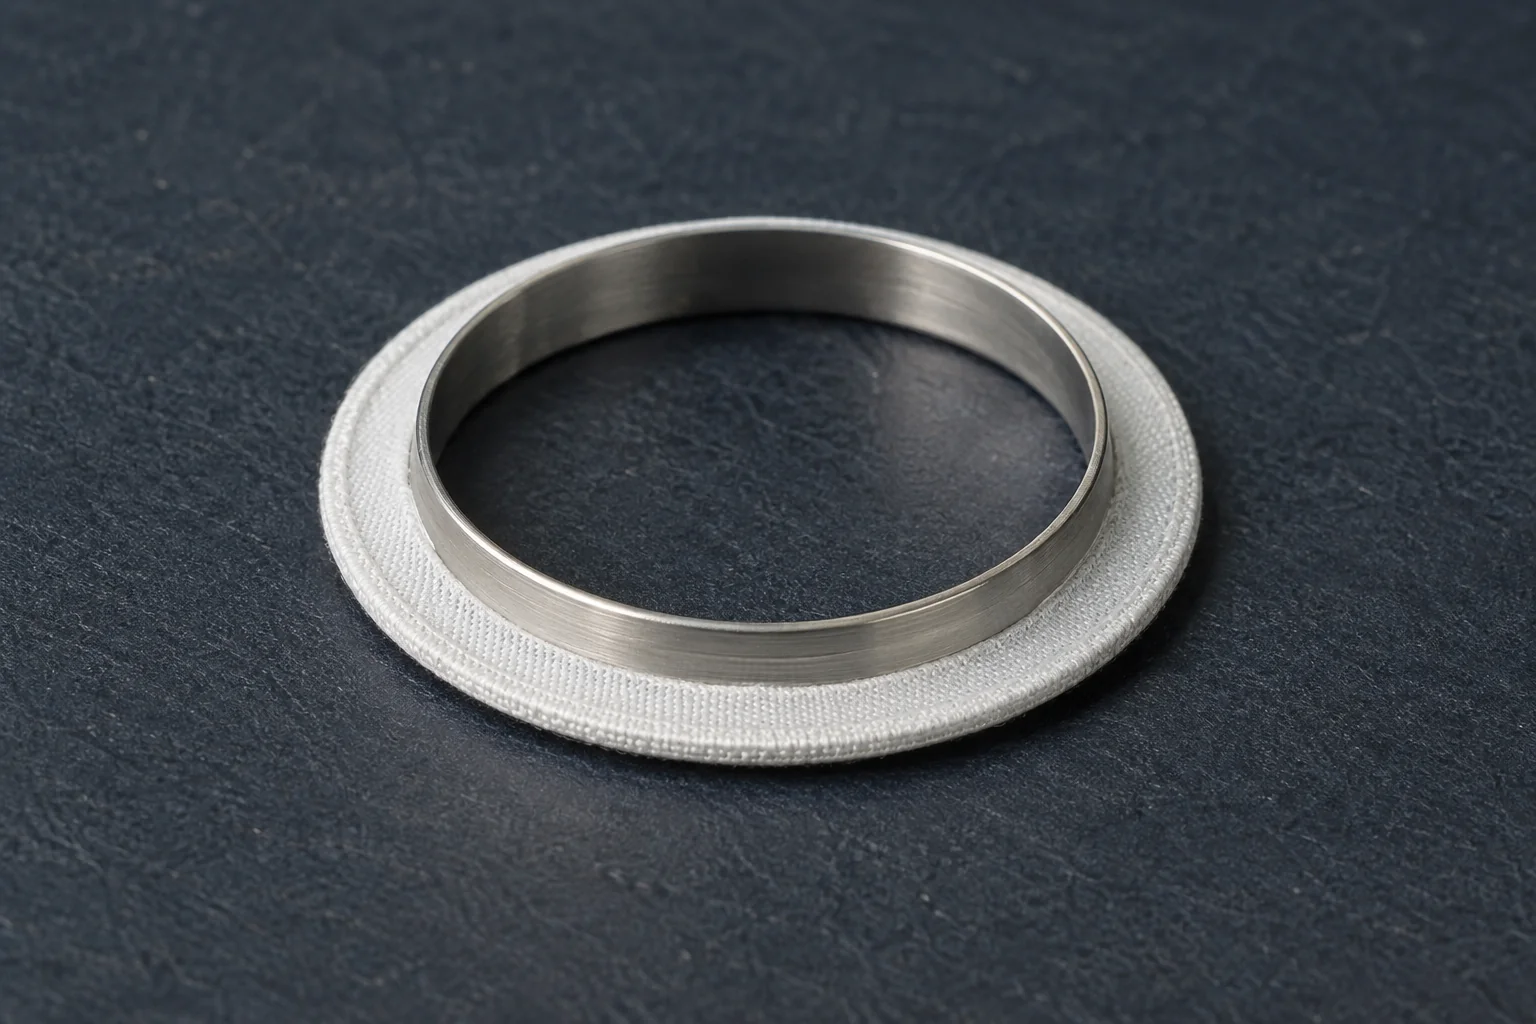
THE DETAIL THAT MATTERS
Material, coverage and seam placement need agreed acceptance criteria. The inspection record connects those requirements to the component.